What Factors Affect Color Consistency in PS Extrusion Compound?
2026-11-11
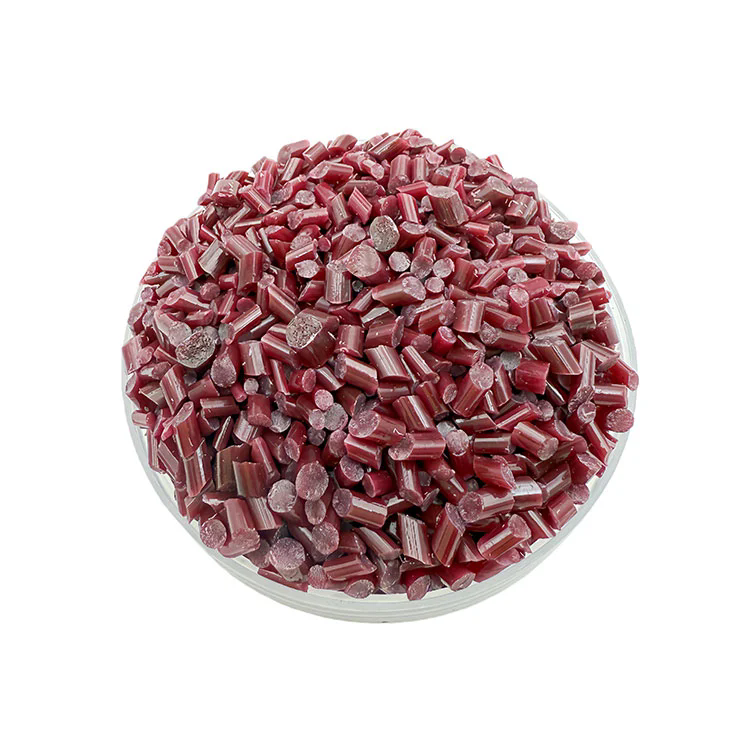
A sheet extrusion plant receives a complaint from a customer who produces refrigerator liners. The customer reports a visible color difference between two deliveries of the same off-white PS Extrusion Compound. The Delta E is 1.8, which is above the 1.0 limit in the specification. The compound supplier checks the formula and finds that the pigment concentration is unchanged. The problem is not the formula. It is the dispersion of the pigment, the carrier compatibility, and the heat history of the two production runs. This guide explains the factors that affect color consistency in PS extrusion compound and how to verify them before shipment.
1. Why Does Pigment Dispersion Determine Whether Two Batches Look the Same?
A colorant in a PS Extrusion Compound is not a dye that dissolves in the polymer. It is a pigment particle that must be dispersed uniformly throughout the polystyrene matrix. If the pigment particles remain as agglomerates, the light reflects differently, and the batch appears darker or more saturated than a batch with well-dispersed particles. The dispersion quality depends on the mixing energy, the mixing temperature, and the wetting agent in the color masterbatch. In our factory, we measure the dispersion with a filter pressure test and with a microscope count of undispersed particles. Ningbo JUWU International Trading Co., Ltd. has been supplying PS extrusion compounds for over 10 years.
The dispersion is also affected by the pigment type. Organic pigments are harder to disperse than inorganic pigments because the organic particles are smaller and have a higher surface energy. A compound with an organic pigment requires a higher mixing energy and a longer residence time than a compound with an inorganic pigment.
2. How Does Carrier Compatibility Affect Color Development?
The color masterbatch that carries the pigment must be compatible with the PS Extrusion Compound. If the carrier is a different polymer, such as a polyethylene-based masterbatch used in a polystyrene compound, the pigment does not distribute evenly. The carrier and the PS may separate during extrusion, and the color appears streaky. The compatible carrier for polystyrene is a polystyrene-based masterbatch or a universal carrier that is designed for styrenic polymers. The table below shows the carrier compatibility for common masterbatch types.
| Masterbatch carrier | Compatibility with PS | Typical defect | Recommended use |
| PS-based | Excellent | None | Standard PS extrusion compound |
| Universal styrenic | Good | Slight gloss variation | Multi-polymer lines |
| PE-based | Poor | Streaks, phase separation | Not recommended for PS |
| EVA-based | Moderate | Color shift at high loading | Limited to low loading |
| ABS-based | Good | Minor thermal shift | High-impact PS blends |
In our factory, we match the carrier to the base polymer and we test the color development in a small extruder before the production run. We also verify the carrier compatibility by checking the melt flow rate of the masterbatch and the compound. A large difference in melt flow rate can cause poor dispersion and color variation. JUWU provides the carrier declaration and the melt flow data with each masterbatch.
3. What Role Does Heat History Play in Color Shift?
Polystyrene is sensitive to heat history. If the compound is extruded at too high a temperature or if it remains in the extruder for too long, the polymer degrades, and the color shifts toward yellow. The shift is caused by the formation of conjugated double bonds in the polymer chain and by the oxidation of the pigment. The heat history is not the same for every batch, because the extruder temperature profile and the residence time vary with the production rate and the equipment condition. In our factory, we record the melt temperature and the residence time for every batch and we correlate them with the color measurement. We also use a thermal stabilizer in the compound to reduce the yellowing. Ningbo JUWU International Trading Co., Ltd. can provide the heat history record with each batch.
The heat history is especially important for light colors. A light beige or off-white compound shows the yellowing more than a dark color. A dark color can hide a small shift, but a light color cannot.
4. How Do Pigment Concentration and Let-Down Ratio Affect Batch-to-Batch Consistency?
The color is achieved by let-down of a color masterbatch into the natural PS Extrusion Compound. The let-down ratio is the weight percentage of the masterbatch in the final compound. A small error in the let-down ratio causes a visible color difference. The let-down ratio must be controlled by a gravimetric feeder with an accuracy of plus or minus 0.5 percent. A volumetric feeder is not accurate enough because the bulk density of the masterbatch varies from batch to batch. The table below shows the effect of let-down ratio error on color difference.
| Let-down ratio error | Color difference (Delta E) | Visibility | Control action |
| ±0.2% | 0.2 – 0.4 | Not visible | None |
| ±0.5% | 0.5 – 0.8 | Slightly visible | Monitor |
| ±1.0% | 1.0 – 1.8 | Visible | Reject or rework |
| ±2.0% | 1.8 – 3.5 | Clearly visible | Reject |
Compound quality engineer's note: The let-down ratio is the most common cause of batch-to-batch color variation in PS extrusion compound. A volumetric feeder that is set by the operator's visual estimate can produce a 2 percent error, which is enough to fail the color specification. In our factory, we use a gravimetric feeder with a closed-loop control and we verify the let-down ratio by weighing a sample of the final compound. JUWU provides the let-down ratio record with each batch.
5. How Should Buyers Specify and Verify Color Consistency in PS Extrusion Compound?
The specification should include five items. The first is the color standard, expressed as a Delta E limit against a master sample. The second is the pigment type and the carrier type. The third is the let-down ratio and the feeding method. The fourth is the heat history limit, including the maximum melt temperature and the maximum residence time. The fifth is the test method, including the spectrophotometer geometry and the illuminant. The verification should include four checks. The first is the color measurement on a molded plaque. The second is the dispersion check with a filter pressure test. The third is the carrier compatibility check with the melt flow rate. The fourth is the batch traceability record. In our factory, we perform these checks on every batch and we provide the color measurement report with the shipment. Ningbo JUWU International Trading Co., Ltd. also keeps a retention sample from each batch for 12 months.
We recommend that the buyer specify the measurement geometry and the illuminant in the purchase order. A color that matches under one illuminant may not match under another. The most common geometry for plastic color measurement is the integrating sphere with a D65 illuminant and a 10 degree observer.
Frequently Asked Questions About Color Consistency in PS Extrusion Compound
Summary for Compound Buyers and Quality Engineers
Color consistency in PS Extrusion Compound is determined by four factors: the pigment dispersion, the carrier compatibility, the let-down ratio, and the heat history. The dispersion must be uniform to avoid agglomerates. The carrier must be compatible with the polystyrene to avoid phase separation. The let-down ratio must be controlled by a gravimetric feeder to avoid concentration errors. The heat history must be recorded and limited to avoid yellowing. The specification should include the color standard, the pigment and carrier types, the let-down ratio, the heat history limit, and the test method. The verification should include the color measurement, the dispersion check, the carrier check, and the batch traceability record. Ningbo JUWU International Trading Co., Ltd. has been supplying PS extrusion compounds for over 10 years and provides full color consistency and traceability support for our customers.