Why Do Different Fibers Need Different Optical Brighteners?
2026-09-29
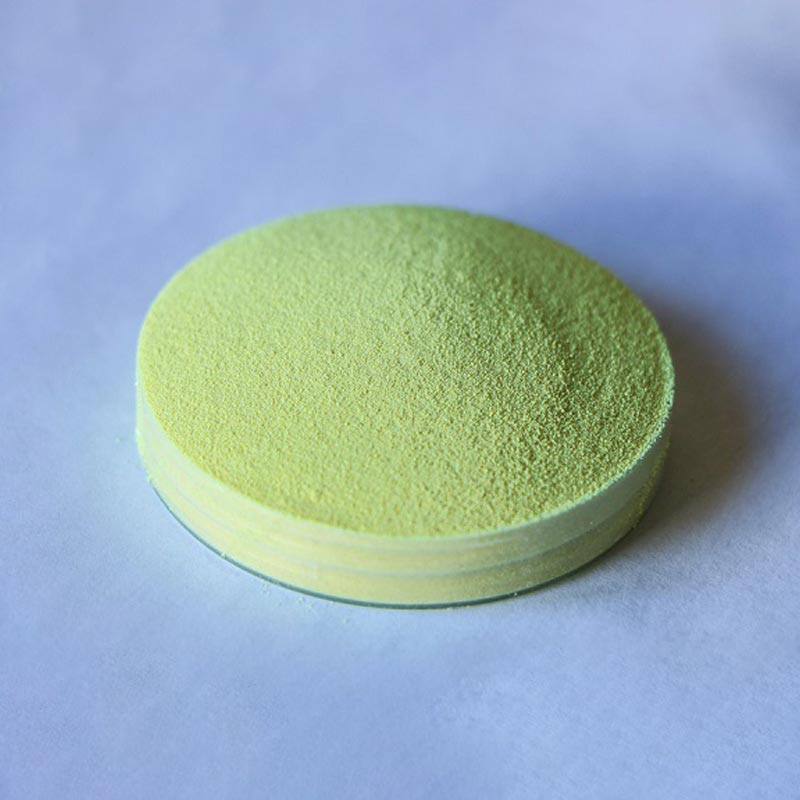
A dyehouse technician runs a white cotton fabric through the padder with an Optical Brightener that has performed well for years. The whiteness is excellent. The next day, the same brightener is used on a polyester blend. The fabric comes out with a dull, yellowish cast instead of a bright white. This is not a dosing error. It is a chemistry mismatch. Optical Brighteners are fluorescent dyes that absorb ultraviolet light and re-emit it as visible blue light. This blue light compensates for the yellow tint of the fiber and makes it appear whiter. But the brightener molecule must attach to the fiber. Cotton, polyester, nylon, and wool have different chemical structures, different surface charges, and different affinities for brightener molecules. This guide explains why the same brightener cannot work on all fibers and how to select the right one for each.
1. Why Does Fiber Chemistry Determine Brightener Selection?
The interaction between an Optical Brightener and a fiber is governed by the same forces that govern dyeing. Cotton is a cellulose fiber with hydroxyl groups that can form hydrogen bonds with brightener molecules. Polyester is a hydrophobic fiber with no reactive groups; the brightener must be dispersed in the fiber matrix. Nylon is a polyamide with amino end groups that can attract anionic brighteners. Wool is a protein fiber with both amino and carboxyl groups. Each fiber requires a brightener with the right molecular size, charge, and solubility. The table below shows the fiber types and their brightener compatibility.
| Fiber type | Chemical nature | Brightener type required | Application method |
| Cotton | Cellulose (hydroxyl groups) | Anionic stilbene derivatives | Exhaust or pad-batch |
| Polyester | Hydrophobic (PET) | Disperse brighteners | High-temperature exhaust or thermosol |
| Nylon | Polyamide (amino groups) | Anionic or cationic brighteners | Exhaust at acidic pH |
| Wool | Protein (amino and carboxyl groups) | Anionic brighteners | Exhaust at acidic pH |
| Acrylic | Polyacrylonitrile | Cationic brighteners | Exhaust at acidic pH |
In our factory, we produce Optical Brighteners for each of these fiber types. The molecular structure is different for each product. A stilbene derivative that works on cotton will not penetrate polyester because the polyester chains are tightly packed and hydrophobic. A disperse brightener that works on polyester will not exhaust onto cotton because it has no affinity for cellulose.
2. How Does the Application Method Affect Brightener Performance?
The application method must match the brightener and the fiber. Cotton brighteners are typically applied by exhaust dyeing at 60°C to 90°C or by pad-batch at room temperature. Polyester brighteners require high temperature (130°C) and pressure to open the fiber structure and allow the disperse brightener to diffuse inside. Nylon and wool brighteners are applied at acidic pH (4 to 5) to promote the attraction between the anionic brightener and the amino groups. The table below shows the recommended application conditions for each fiber type.
| Fiber | pH | Temperature | Time | Typical concentration |
| Cotton | 7 – 9 | 60 – 90°C | 30 – 60 min | 0.1 – 0.5% owf |
| Polyester | 4 – 6 | 130°C | 30 – 45 min | 0.2 – 1.0% owf |
| Nylon | 4 – 5 | 60 – 80°C | 30 – 45 min | 0.1 – 0.3% owf |
| Wool | 4 – 5 | 50 – 70°C | 30 – 60 min | 0.2 – 0.8% owf |
| Acrylic | 3 – 5 | 70 – 90°C | 30 – 60 min | 0.1 – 0.5% owf |
Hangzhou Tongge Energy Technology Co., Ltd. manufactures Optical Brighteners for all of these fiber types. Our factory provides detailed application guidelines with each product. We also offer a technical service that helps customers optimize the concentration, pH, and temperature for their specific equipment and water quality.
3. What Happens When the Wrong Brightener Is Used?
Using the wrong brightener produces one of three outcomes. The first is no whitening effect. The brightener does not attach to the fiber, so it is washed away during rinsing. The fabric remains yellow. The second is uneven whitening. The brightener attaches to some areas of the fabric but not others, producing a blotchy appearance. This is common when a cotton brightener is used on a polyester-cotton blend; the brightener goes to the cotton but not the polyester. The third is yellowing. Some brighteners oxidize or degrade under the wrong conditions and produce a yellow color instead of a blue-white. This is often seen when a disperse brightener is used on nylon at high temperature. The table below summarizes these failure modes.
| Failure mode | Cause | Symptom | Corrective action |
| No whitening effect | Brightener has no affinity for fiber | Fabric remains yellow | Switch to the correct brightener type |
| Uneven whitening | Blend fiber competition | Blotchy appearance | Use a blend-specific brightener |
| Yellowing | Brightener degradation | Yellow cast instead of white | Reduce temperature or change brightener |
| Poor wash fastness | Brightener not fixed | Whiteness fades after washing | Adjust pH or use a fixing agent |
Technician's tip: Before running a production batch, always perform a lab dip with the actual fiber and the intended brightener. A 5-gram sample costs almost nothing and can prevent a 500-meter production error.
4. How Should Brighteners Be Selected for Fiber Blends?
Fiber blends are common in modern textiles. A 65/35 polyester-cotton blend contains both hydrophobic polyester and hydrophilic cotton. No single brightener works on both fibers. The solution is to use a combination of brighteners: a disperse brightener for the polyester and a cotton brightener for the cellulose. The two brighteners must be compatible with each other and with the application conditions. In our factory, we offer a range of blend-specific Optical Brighteners that are formulated with both types of active ingredients. These products provide uniform whiteness across the blend without the need for two separate application steps. For a 50/50 blend, we recommend a one-bath application with a dual-action brightener. For a 65/35 blend, a two-bath application may be more effective.
Frequently Asked Questions About Optical Brighteners for Different Fibers
Summary for Textile Technicians and Dyehouse Managers
Different fibers need different Optical Brighteners because the brightener molecule must attach to the fiber through chemical or physical forces. Cotton requires anionic stilbene derivatives, polyester requires disperse brighteners, nylon and wool require anionic brighteners, and acrylic requires cationic brighteners. Using the wrong brightener results in no whitening, uneven whitening, or yellowing. For blends, a combination of brighteners or a dual-action product is required. Hangzhou Tongge Energy Technology Co., Ltd. has been manufacturing Optical Brighteners for over 12 years and supplies to textile mills worldwide.
Hangzhou Tongge Energy Technology Co., Ltd. manufactures Optical Brighteners for cotton, polyester, nylon, wool, and acrylic fibers. We provide full application guidelines and technical support for our products.